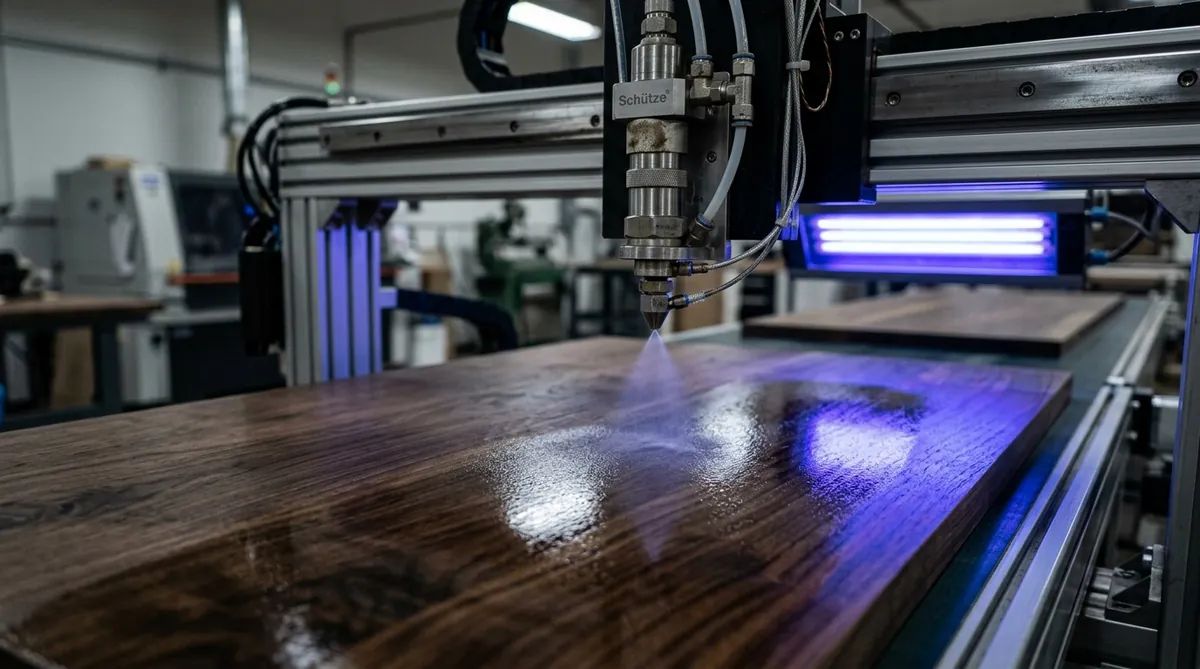
A finish is qualified by what it looks like after twenty-four hours of contact, not by how it photographs on handover day. Housekeeping wipes guestroom casework with 75% alcohol several times a day, luggage wheels strike the same plinth edge at every changeover, and in a subtropical climate the film takes UV through the window for the life of the asset. Ordinary nitrocellulose and low-crosslink polyurethane finishes begin to whiten, soften and lift at the edges somewhere between month six and month twelve of operation. Once the film is breached, moisture reaches the substrate and the failure stops being cosmetic.
This article covers the four-coat system Sunder specifies for contract work, and — more usefully during a tender — the four test standards that separate a finish that will hold from one that will not.
1. How Conventional Films Fail: Hydrolysis and Abrasion
Residential-grade coatings fail in commercial cleaning regimes by a predictable route. Low crosslink density lets solvent swell the polymer network; unsealed capillary pores let moisture reach the wood fibre underneath.
+-------------------------------------------------------------------------+
|        Conventional film vs high-crosslink coating: reaction path       |
+-------------------------------------------------------------------------+
|  [Contact media] 75% alcohol / 0.5% sodium hypochlorite / wine, coffee  |
|        |                                                                |
|        +--> [Conventional NC or standard PU film]                       |
|        |     Low crosslink density -> solvent swells film -> whitening, |
|        |     tack, edge lift                                            |
|        |     Open capillary pores -> moisture reaches substrate ->      |
|        |     fibre swelling, mould, replacement                         |
|        |                                                                |
|        +--> [UV-cured PU, high crosslink density]                       |
|              Dense three-dimensional network -> pore closure ->         |
|              no film change after 24h contact (ASTM D1308)              |
|              Surface hardness >= 3H -> luggage contact leaves no mark   |
+-------------------------------------------------------------------------+
Yellowing follows a separate mechanism. Aromatic polyurethanes shift colour under UV; aliphatic systems with a UV absorber do not, and the difference is measurable rather than a matter of opinion.
+-------------------------------------------------------------------------+
|            ASTM G154 QUV accelerated weathering, colour shift           |
+-------------------------------------------------------------------------+
|  Colour shift (Delta E)                                                 |
|    ^                                                                    |
|  6 |                  [Conventional clear coat] -> Delta E >= 5.5 at    |
|    |               /                                300 hours           |
|  4 |     /                                                              |
|    |----/-------------------------------------- (visible yellowing)     |
|  2 |                                                                    |
| 1.5|---[Aliphatic PU with UV absorber] ========= (Delta E <= 1.5 at     |
|    |                                              500 hours)            |
|   0+----------------------------------------------------> Exposure hrs  |
|         0 h                        250 h                    500 h       |
+-------------------------------------------------------------------------+
2. The Four-Coat Enclosed System
The objective is to keep the grain of a natural veneer visible while closing the surface completely. Four coats, applied in an automated dust-free line:
+-------------------------------------------------------------------------+
|              Four-coat build, cross-section (top to bottom)             |
+-------------------------------------------------------------------------+
|  [Layer 1] Matte topcoat: two-part high-crosslink PU with nano-ceramic  |
|            particles, 3H                                                |
|                                |                                        |
|  [Layer 2] Anti-yellowing mid-coat: aliphatic polyurethane clear with   |
|            UV absorber                                                  |
|                                |                                        |
|  [Layer 3] Sealing primer: UV-cured acrylic, fills capillary pores      |
|                                |                                        |
|  [Layer 4] Substrate: 0.6mm selected veneer over E0 / JIS F four-star   |
|            moisture-resistant plywood                                   |
+-------------------------------------------------------------------------+
1. Total film build: 120 to 150 µm
Primer, mid-coat and topcoat are sprayed to a controlled dry film thickness of to . That is what closes the veneer’s capillary pores; below roughly 100 µm the pores stay open regardless of the chemistry above them.
2. Surface hardness: ASTM D3363 at 3H or above
Nano-alumina () in the topcoat raises pencil hardness to under ASTM D3363. Abrasion is verified separately under ASTM D4060 (Taber, CS-10 wheel, 1,000 g load, mass loss at 1,000 cycles).
A caveat worth stating: 3H resists the contact a luggage wheel or a key makes in normal use. It is not a claim about deliberate gouging, and no furniture-grade finish should be specified as though it were.
3. Chemical resistance: ASTM D1308, 24-hour contact
Before shipping, the coating is held in continuous contact for 24 hours with:
- 75% medical alcohol, sodium hypochlorite solution, hot coffee, red wine, citric acid
and assessed against ISO 2812 / ASTM D1308 at rating 0 — no softening, no whitening, no gloss loss.
3. Acceptance Matrix Against International Standards
Surface coating inspection items and qualifying standards
| Inspection item | Test method | Qualifying result |
|---|---|---|
| Pencil hardness | ASTM D3363 / JIS K5600 | >= 3H, no indent or mark |
| Film adhesion | ASTM D3359 cross-hatch | Class 5B, 0% removal |
| Chemical resistance | ASTM D1308 spot, 24h | Rating 0 |
| Abrasion | ASTM D4060 Taber | <= 40 mg at 1,000 cycles |
| QUV weathering | ASTM G154, 500 hours | Delta E <= 1.5 |
| Formaldehyde / VOC | JIS A 1460 chamber | JIS F four-star, <= 0.3 mg/L |
Ask for the report, not the claim. Each of these is a numbered method with a pass criterion, and a supplier who has run them can produce the certificate.
4. Surface Friction and Housekeeping OpEx
Closing the pores changes daily cleaning as much as it changes durability.
+-------------------------------------------------------------------------+
|            Closed-pore finish: effect on housekeeping and asset         |
+-------------------------------------------------------------------------+
|  [Wiping resistance]  Smooth, pore-free surface -> less cloth drag,     |
|                       single-pass wiping                                |
|                                                                         |
|  [Stain behaviour]    Oil and water repellent -> dried coffee and wine  |
|                       lift with a damp cloth, without solvent           |
|                                                                         |
|  [Refinishing]        3H film -> on-site touch-up is not part of the    |
|                       normal maintenance cycle, so rooms stay sellable  |
+-------------------------------------------------------------------------+
5. Manual Brush Finishing vs UV-Cured Line: Ten-Year Comparison
The figures below are a modelled comparison, not a measurement. They assume a 300-key property on a standard housekeeping regime with daily alcohol wiping; substitute your own refinishing cycle and the totals move, though the ordering generally does not.
Surface coating: manual brush finishing vs automated UV-cured
| Evaluation vector | Manual / residential | UV-cured line |
|---|---|---|
| Surface hardness | HB to 1H | 3H (ASTM D3363) |
| Alcohol contact | Whitening and tack reported within months | Rating 0 at 24h (ASTM D1308) |
| UV colour shift | Visible yellowing | Delta E <= 1.5 at 500h |
| Refinishing cycle | Spot respray every 1 to 2 years | Not scheduled within the 10-year model |
| Finish-related complaints | Recurring in guest feedback | Not a recurring category |
| 10-year modelled cost | Baseline, plus refinishing | Roughly one third of baseline |
6. Conclusion: Specify the Test, Not the Adjective
The furniture surface is the interface a guest touches most and looks at longest. Structure and veneer selection do not survive a cleaning regime on their own — the film above them does.
The practical takeaway for a specification is narrow. Name the four methods (ASTM D3363, D1308, D4060, G154), state the pass criterion for each, and require the reports at the sample-approval stage rather than after delivery. A finish that cannot produce them is not necessarily poor, but it is unverified, and on a ten-year asset that distinction is the whole decision.